


Views: 0 Author: Site Editor Publish Time: 2026-10-08 Origin: Site


High-gloss finishes leave zero room for error. Even microscopic variations reflect light irregularly across the surface. These visual imperfections quickly lead to rejected parts. Consequently, they escalate scrap costs and disrupt production schedules. Producing flawless cosmetic components requires a delicate balance. You need tooling precision, polymer science, and strict process control. Standard molding tolerances fall short when assessing optical quality. Manufacturers must tightly control every single variable. This rigorous control ensures a perfect, mirror-like finish every time. This guide breaks down the root causes of gloss inconsistencies. It helps you understand exactly where processes fail during production. You will learn a systematic framework for evaluating your tooling and processing parameters. We will also help you assess manufacturing partnerships effectively. By applying these exact principles, you can eliminate surface blemishes entirely.
Cosmetic finishes heavily influence consumer perception and purchasing decisions. High-gloss parts are typically highly customer-facing. You find them frequently in consumer electronics, premium packaging, and automotive interiors. When consumers see a dull spot, flow line, or scratch, they immediately question product quality. Surface flaws directly impact perceived brand value and market positioning.
Uncontrolled processes lead to immense financial waste. Scrap rates for cosmetic components can easily exceed 15-20%. This happens when manufacturers fail to dial in the injection process properly before full-scale production. Rectifying these issues mid-production is notoriously difficult. Reworking hardened, high-polish steel molds is exceptionally expensive. It requires specialized diamond buffing by master toolmakers. Tooling modifications also cause severe delays in time-to-market. Managing high gloss injection molding defects proactively is essential for stable, profitable production runs.
Predictable cosmetic yields define a successful manufacturing operation. You must move away from trial-and-error machine setups. Instead, adopt scientific molding principles from day one. Engineers should conduct upfront mold flow analysis on every cosmetic part. This simulation software identifies potential problem areas before cutting any steel. Predictive analysis guarantees repeatable cosmetic yields and protects long-term profit margins.
Surface blemishes rarely result from a single arbitrary error. They usually stem from a complex combination of material handling, tool design, and processing parameters.
Improper material handling guarantees poor surface finishes. Polymers require highly specific conditions before they enter the injection barrel.
Best Practice: Always use automated desiccant dryers for hygroscopic materials. Monitor dew points continuously to ensure optimal, consistent drying environments.
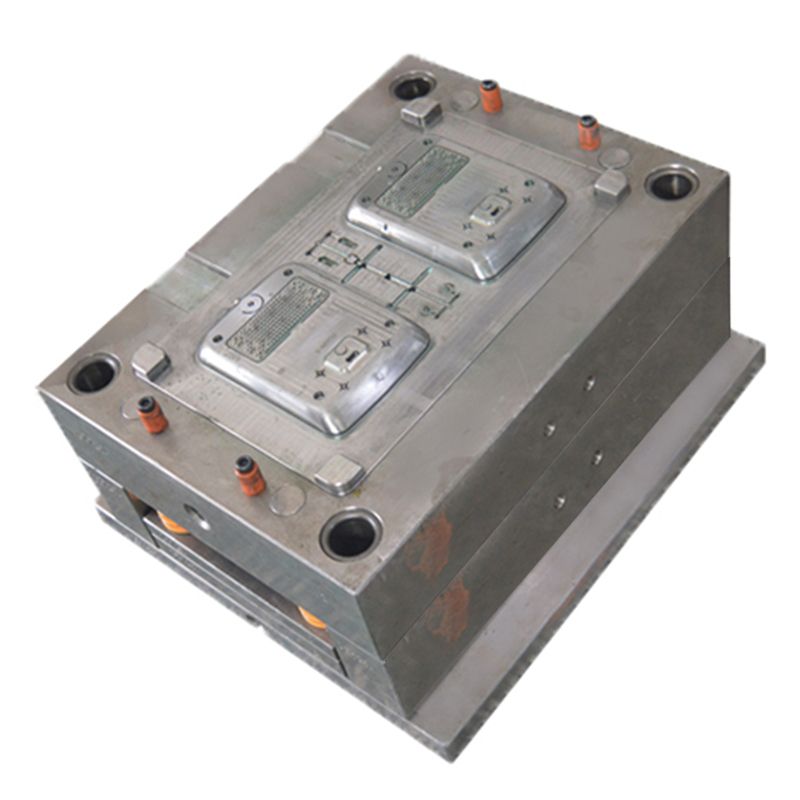
The mold itself fundamentally dictates the final part appearance. Even perfectly prepared resins fail visually in poorly designed tools.
Common Mistake: Relying on standard, out-of-the-box venting depths for high-viscosity materials. Always customize venting strategies based on specific polymer flow rates and part geometry.
Operators must balance thermal and kinetic energy flawlessly during production. Arbitrary machine adjustments often worsen existing cosmetic issues.
Clear components demand the absolute highest level of manufacturing rigor. Standard opaque molding rules do not fully apply to these transparent applications.
Optical vs. Cosmetic Standards:
Clear applications include optical lenses, automotive light pipes, and medical display screens. These complex products require flawless external surface gloss. However, they also require perfect internal optical clarity. Engineers measure this internal clarity as low birefringence. High birefringence indicates internal molded-in stress, which bends transmitted light unpredictably. Achieving both external gloss and internal clarity requires perfect thermodynamic balance. Producing flawless high-gloss clear plastic parts demands extreme precision in mold temperature control.
Shear Stress Sensitivity:
Clear polymers are highly sensitive to aggressive processing environments. Polymethyl Methacrylate (PMMA) and Polycarbonate (PC) react poorly to high shear stress. Shear stress manifests as physical structural weakness. More importantly, it creates intense visual distortion under direct lighting. Operators must continuously optimize injection speeds to minimize this shear friction during the fill phase.
Contamination Risks:
Opaque masterbatches hide minor imperfections easily. Clear parts offer absolutely no such forgiveness. Minor black specks or carbon buildup instantly ruin a clear component. Yellowing from subtle thermal degradation is immediately visible to the naked eye. The entire manufacturing environment must robustly support contamination control. Purging compounds must be perfectly matched to the specific clear resin type.
Troubleshooting cosmetic flaws requires a strict, evidence-based approach. Guesswork on the production floor destroys tooling and inflates overall production costs.
Evidence-Based Auditing:
Avoid temporary quick fixes on the production floor. Aerosol mold release sprays represent a major process failure. They instantly ruin surface gloss by leaving a chemical film. They also complicate secondary operations like painting, plating, or pad printing. You must audit the root mechanical or thermal cause instead.
Tooling Polish Standards:
High-gloss parts require very specific, highly engineered tooling finishes. Verify your mold finishes meet SPI A-1 or A-2 industry standards. Toolmakers achieve this extreme smoothness using ultra-fine diamond buffing. Furthermore, ensure the tool steel is appropriately hard. Premium steels like H13 or S136 resist long-term wear and deformation. They maintain their high polish over high-volume production runs. Softer metals degrade quickly under intense injection pressure.
Thermal Management Tech:
Standard cooling channels often fall short for ultra-high gloss requirements. Evaluate dynamic mold temperature control systems. Technologies like Variotherm or Rapid Heat Cycle Molding (RHCM) offer distinct thermodynamic advantages. They maintain high cavity heat during the entire injection phase. This high heat maximizes precise surface gloss replication. Once filled, the system initiates rapid, aggressive cooling. Rapid cooling preserves efficient cycle times without sacrificing optical quality.
Design of Experiments (DOE):
You must isolate processing variables systematically. Adjusting multiple machine parameters simultaneously masks the true root cause of a defect. A structured Design of Experiments (DOE) framework is essential for scientific molding. Isolate melt temperature, mold temperature, and pack pressure independently. Document the visual results meticulously. This analytical method reveals the exact optimal process window for your part.
| Defect Type | Primary Variable to Check | Immediate Corrective Action |
|---|---|---|
| Splay (Silver Streaks) | Material Moisture Level | Verify dryer dew point; extend drying time appropriately. |
| Gate Blush | Injection Speed / Gate Size | Profile injection speed slower at the gate; open gate geometry. |
| Dull Surface / Flow Marks | Mold Temperature | Increase mold temperature to delay premature melt freezing. |
| Burn Marks (Diesel Effect) | Venting / Clamping Force | Clean existing vents thoroughly; reduce clamp tonnage slightly if over-clamped. |
Partnering with the wrong manufacturing vendor guarantees project failure. Commodity molders often lack the required infrastructure for high-end cosmetic production.
Implementation Risks:
Commodity molders inherently focus on rapid cycle times over surface aesthetics. They often compromise on tooling steel quality to win competitive bids. This short-sighted approach leads to rapid tool degradation and incredibly high scrap rates. Effectively avoiding high gloss injection molding defects requires a specialized, highly technically competent partner.
Evaluation Dimensions:
Evaluate potential partners rigorously across three critical dimensions.
Red Flags to Watch For:
Be extremely wary of vendors guaranteeing zero defects upfront without data. If they skip comprehensive Moldflow analysis, they are merely guessing. Another major red flag is post-mold masking. Vendors who recommend painting to cover molding defects lack underlying process control. Painting adds unnecessary cost, creates environmental hazards, and rarely fixes the underlying structural weakness.
Surface defects in high-gloss injection-molded parts are entirely preventable. However, this prevention requires rigorous upfront engineering and planning. You must invest heavily in flawless tool steel and advanced thermal management systems. Strict, scientific process control guarantees repeatable cosmetic yields across thousands of cycles.
The absolute cheapest tooling quote often becomes a massive liability. Skimping on mold polish quality or complex cooling layouts ensures an expensive, frustrating production run. Cosmetic finishes demand precision at every single step of the manufacturing value chain.
Protect your brand reputation proactively from the start. Consult our engineering team for a comprehensive DFM review today. We provide thorough tooling audits to ensure your high-gloss components are designed perfectly for manufacturability. Partner with us to guarantee consistent, defect-free cosmetic yields.
A: Dull spots near the gate usually indicate excessive shear stress. As plastic forces its way through a narrow gate, high friction alters the melt properties. You can solve this by adjusting the injection speed profile to fill slower initially. Enlarging the gate geometry or increasing the mold temperature also reduces this shear friction significantly.
A: Mold temperature is the primary driver of surface finish replication. Higher mold temperatures keep the plastic melt in a liquid state longer. This extended liquid phase allows the polymer to pack tightly against the polished steel cavity. Slower freezing drastically reduces flow lines, ensuring a highly reflective, uniform gloss.
A: You can sometimes minimize minor sink marks by increasing holding pressure and extending cooling time. However, severe sink marks stem from poor core geometry. Thick rib-to-wall ratios cause uneven shrinkage during the cooling phase. Permanent resolution usually requires a design adjustment to hollow out thick sections or reduce rib thickness.
A: Cloudiness and yellowing have distinct root causes. Cloudiness is typically a mechanical issue related to cold mold temperatures or degraded tooling polish. Yellowing almost always indicates chemical material degradation. This degradation occurs due to excessive barrel heat, prolonged residence time, or inadequate drying of hygroscopic resins before injection.


